

Plastic recycling can reduce the need to extract and process virgin raw materials, which is why recycling is associated with lifecycle energy savings. Inside a recycling plant, however, electricity, heat and water still have to be managed carefully. Sorting, shredding, washing, drying and pelletizing all consume energy, and the lowest motor rating does not automatically produce the lowest operating cost.
For equipment buyers, the practical measure is energy per unit of saleable output. Track kWh per input ton, kWh per good-output ton, reject rate, moisture, uptime and labor together. A line that uses less power but produces unstable or contaminated material may be less efficient overall.
I’m Jacky, CEO of AMIGE. When we discuss energy-efficient plastic recycling, I prefer to start with a material balance and process map. That shows where energy is used, where material is lost and which machine is limiting the whole line.
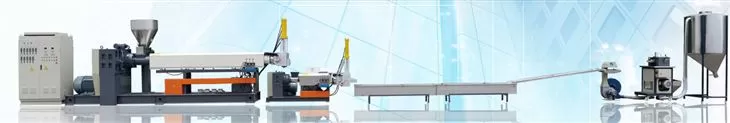
How does plastic recycling save energy?
Using recovered plastic can avoid parts of the virgin-material chain, including raw-material extraction and primary resin production. Mechanical recycling usually keeps the polymer in use through sorting, cleaning, size reduction and remelting. The actual lifecycle benefit depends on resin, contamination, collection, transport, process yield, electricity source and the product that the recycled material replaces.
This is why a fixed energy-saving percentage should not be promised for every project. Compare equivalent system boundaries and final products. For plant purchasing, also separate lifecycle savings from the facility’s own electricity and thermal demand.
Where does a recycling line use energy?
| Process stage | Main energy demand | Efficiency opportunity |
|---|---|---|
| Sorting and feeding | Conveyors, separators and compressed air | Stable feed and early contaminant removal |
| Shredding or crushing | Cutting motor and recirculation | Correct cutter, clearance and output size |
| Washing | Pumps, friction and water heating | Match cleaning intensity to contamination |
| Drying | Mechanical and thermal moisture removal | Remove water mechanically before applying heat |
| Pelletizing | Extruder drive, heaters, filtration and cutting | Stable feed, correct temperature and clean screens |
| Utilities | Cooling, air, water treatment and dust control | Measure and control auxiliaries as part of the line |
Seven ways to reduce energy per ton
1. Remove contamination before it consumes process energy
Metal, stones, excessive dirt and incompatible polymers use machine time and energy but do not become saleable product. Early inspection and separation protect equipment and improve good-output yield.
2. Avoid unnecessary size reduction
Smaller particles are not always better. An overly small screen can increase recirculation, dust, heat and knife wear. Specify the largest particle size that still works reliably in washing, separation or extrusion.
3. Keep cutters sharp and clearances correct
Dull knives tear and rub rather than cut cleanly. Monitor amperage, vibration, flake quality and capacity, then maintain knives and screens before poor cutting raises energy per useful ton.
4. Match washing intensity to contamination
Not every stream needs the same residence time, water temperature or friction. Define the incoming contamination and final specification, then select cold washing, hot washing and friction washing accordingly.
5. Remove moisture mechanically before thermal drying
Mechanical dewatering can remove bulk water before heated air finishes the job. Measure moisture between stages so the thermal dryer is not compensating for poor upstream drainage or dewatering.
6. Stabilize extruder feeding and filtration
Variable feed, moisture and contamination can increase motor load, heater demand, pressure fluctuation and screen changes. A stable prepared feed helps an industrial plastic pelletizer operate closer to its intended process window.
7. Balance the complete line
A large motor is not efficient if the next machine repeatedly stops it. Size the shredder, washer, dryer and pelletizer around the same realistic material flow. Use buffers and controls where they prevent stop-start operation without hiding a permanent bottleneck.
How to compare energy-efficient recycling equipment
- Ask for a representative material test and defined system boundary.
- Record input tons, good output, rejects and operating time.
- Measure the complete line, including heaters, pumps, dryers and auxiliaries.
- Compare kWh per good-output ton, not installed kW alone.
- Check moisture, contamination and product quality at the same time.
- Review idle power, startup, stoppages and cleaning losses.
- Confirm voltage, frequency, ambient conditions and local utility cost.
- Request motor, control, maintenance and spare-part documentation.
Installed power indicates the possible electrical load; it does not equal constant consumption. Actual energy depends on motor loading, heater duty, material, output, control logic and operating condition. A supplier should explain the assumptions behind any consumption estimate.
Information needed for an energy and cost review
Send the material type and condition, hourly input, target output quality, contamination, moisture, operating hours, local electricity and water conditions, available factory space and current process if one exists. Photos, videos and a representative sample make the review more useful.
AMIGE can map the required plastic washing line, size-reduction and pelletizing stages around the feed and output target. The result should be a balanced process with measurable performance conditions.
Frequently asked questions
Does recycling plastic always save energy?
Recycling can avoid energy used in virgin-material production, but the result depends on polymer, collection, transport, contamination, process yield, energy source and the product displaced. Compare equivalent lifecycle boundaries.
What is the best energy metric for a recycling plant?
Use kWh per ton of saleable output together with yield, moisture, quality, uptime and labor. Installed power or kWh per input ton alone can hide reject losses and unstable production.
Does a smaller crusher screen use more energy?
It can increase recirculation, heat and cutting work, depending on material and machine design. Select the output needed by the next stage and verify capacity and energy during a test.
Which recycling stage uses the most energy?
There is no universal answer. Contamination, moisture, washing temperature, drying method, extrusion and auxiliaries change the balance. Meter major stages to identify the actual constraint.
How can buyers verify a supplier’s energy claim?
Request test conditions, material, run time, good output, rejects, moisture, quality and the equipment included in the measurement. Confirm whether the figure covers the complete line or one motor.
Conclusion
Plastic recycling can support lifecycle energy savings, while plant efficiency depends on yield and balanced equipment. Measure the complete process, remove non-value work and compare energy per saleable ton before choosing machinery.
