

An industrial conveyor system moves plastic scrap or processed flakes between recycling stages at a controlled rate. A motor drives the belt or chain, while pulleys, rollers, supports and sensors keep the material moving toward the shredder, crusher, washer, dryer or storage bin.
The conveyor is part of the process control—not just transportation. If it feeds too quickly, the next machine overloads. If it feeds too slowly or allows bridging, the line loses capacity.
I’m Jacky, CEO of AMIGE. When we design a recycling line, the conveyor must match material shape, bulk density, moisture, incline, required throughput and the receiving machine’s loading behavior.
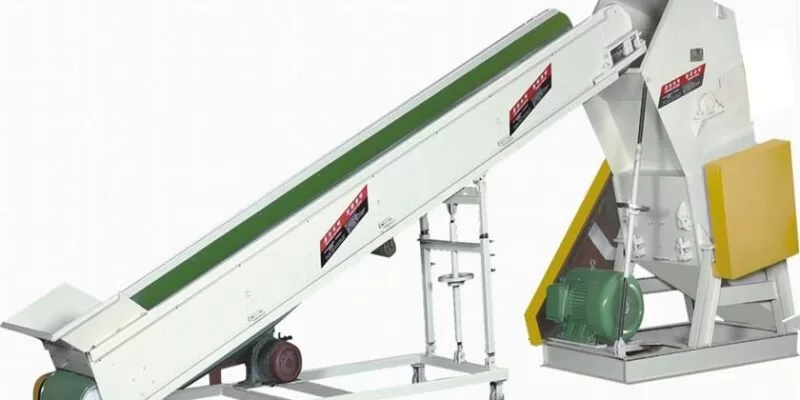
How an Industrial Belt Conveyor Works
An electric motor and gearbox rotate the drive pulley. Friction between that pulley and the belt creates movement. An idler or tail pulley returns the belt, while rollers or a slider bed support it along the carrying and return paths.
Tension keeps the belt engaged and tracking correctly. Scrapers, sidewalls, cleats and covers may be added according to the material and incline. A variable-frequency drive can adjust feeding to the load of the downstream machine.
Where Conveyors Are Used in Plastic Recycling
| Location | Material | Design priority |
|---|---|---|
| Sorting to shredder | Bulky parts, bags or containers | Stable feeding and operator safety |
| Shredder to crusher | Coarse pieces | Prevent surge loading and metal carryover |
| Crusher to washer | Flakes with dirt or moisture | Contain leakage and match washer capacity |
| Washer to dryer | Wet flakes or film | Corrosion resistance and drainage |
| Dryer to storage | Light dry flakes | Dust containment and controlled discharge |
Choosing Belt, Cleats and Sidewalls
A flat belt may suit stable rigid parts on a low incline. Cleats help prevent bottles, lumps or flakes from sliding backward. Sidewalls limit material loss, while covered or enclosed sections can reduce wind and dust exposure.
The belt material must suit abrasion, oil, water, temperature and cleaning chemicals. Wet washing lines may require corrosion-resistant frames, drainage and bearings protected from contamination.
Incline, Speed and Capacity
Conveyor capacity depends on usable belt width, speed, loading depth, bulk density, incline and material behavior. Light film can occupy high volume at low mass, while dense purgings create higher structural and drive loads.
A steeper incline can save floor space but may require cleats, sidewalls or a different conveyor type. Capacity should be confirmed with the real material rather than calculated from weight alone.
Controls and Line Integration
- Interlock conveyor operation with the receiving machine.
- Use motor-current, level or pressure signals to control feed rate.
- Stop upstream feeding when the downstream machine trips.
- Coordinate metal detection or magnetic separation where required.
- Provide restart logic that avoids sending a material surge.
- Define local and central emergency-stop behavior.
The objective is a stable line, not the highest independent conveyor speed. Buffering and controlled starts can prevent blockages after short stops.
Conveyor Safety Requirements
- Guard pulleys, rollers, chains and other nip points.
- Prevent access to hazardous loading and discharge areas.
- Install reachable emergency stops or pull cords as required.
- Apply lockout/tagout before cleaning, tracking or maintenance.
- Control falling material, dust, water and housekeeping hazards.
- Provide safe platforms where routine inspection is necessary.
Final guarding and controls must comply with the installation country and the risk assessment for the complete line.
Maintenance and Common Conveyor Problems
Belt mistracking may come from uneven loading, buildup, damaged rollers, poor alignment or incorrect tension. Slippage can indicate insufficient tension, a contaminated pulley or overload. Spillage usually points to poor loading geometry, inadequate sidewalls or excessive speed.
Inspect belt condition, joints, rollers, bearings, scrapers, guards, sensors and drive components. Record motor current and tracking changes before a failure stops the full recycling line.
How to Specify a Recycling Conveyor
Provide the material, largest item, bulk density, moisture, contamination, required capacity, loading method, discharge height, horizontal distance, incline, operating hours, cleaning method, voltage and line-control requirements.
Conveyors are normally specified together with the receiving equipment. Review the AMIGE plastic crusher and plastic washing line platforms, then send the complete layout through the AMIGE inquiry form.
Frequently Asked Questions
How does an industrial conveyor system work?
A motor drives a belt or chain over pulleys and supports, moving material between process stages at a controlled speed.
Which conveyor is used for plastic recycling?
Belt conveyors are common, but the belt, cleats, sidewalls, incline and frame must match the plastic form, moisture and receiving machine.
How is recycling-conveyor capacity calculated?
It depends on belt width, speed, loading depth, bulk density, incline and material behavior, verified with representative feed.
Why should a conveyor be interlocked with a crusher?
The interlock stops or slows feeding when the crusher overloads or trips, reducing jams and material buildup.
What information is needed to select an industrial conveyor?
Provide material, dimensions, bulk density, moisture, capacity, loading and discharge points, incline, cleaning method, controls and layout.
